

Suppliers can send perfect PDFs. But buyers still receive bad shipments. So I stop trusting brochures first.
Instead, I ask for one Unedited Job Record Pack. Then I decide if “quality” exists on the shop floor.
I have sourced stamping, CNC, and casting for decades. So I trust evidence more than promises.
If your paperwork looks too clean, I get nervous. Because real production leaves fingerprints.
What is a Job Record Pack?
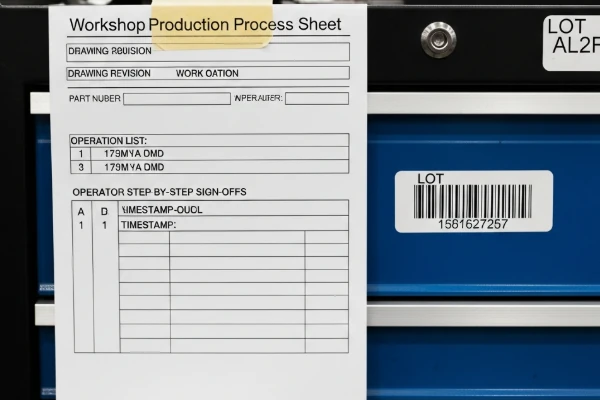
A Job Record Pack is a complete, unedited set of production records from one finished shipment. It links the Purchase Order (PO), drawing revision, material heat number, in-process inspection data, and gauge calibration to the physical shipment labels to prove traceability.
Why messy handwriting beats clean templates in real sourcing
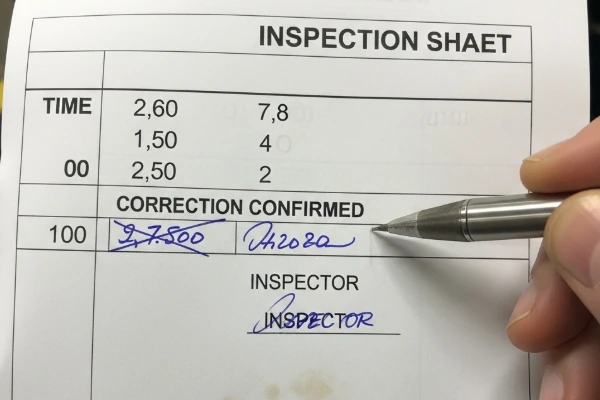
I want oily fingerprints on the inspection sheet. Also, I want a rushed signature from second shift.
And I want a heat number that matches the label on the carton. So I can trace one part to one melt.
Clean templates can hide late backfilling. But messy notes often prove real-time control.
So I look for corrected entries with a signature. Then I trust the data more.
The Essential 25 checklist buyers actually use
I keep the “25 documents” idea. But I split it into two levels. So the list stays usable.
Level 1 proves system discipline. Level 2 proves shop-floor execution.
Level 1: System Control Documents
- ISO 9001 Certificate — verify scope, site, and expiration.
- Quality Manual — confirm it matches real processes.
- Document Control Procedure — confirm revision approvals and release rules.
- Record Retention Procedure — confirm integrity, access, and retention time.
- Training Matrix — confirm station-level training coverage.
- Incoming Inspection Standard — confirm sampling and acceptance criteria.
- Traceability Procedure — confirm heat/lot rules and label rules.
- Material Control Procedure — confirm receiving, storage, and issue logs.
- Calibration Procedure — confirm intervals and traceable standards.
- NCR Procedure — confirm containment and disposition steps.
- CAPA Procedure — confirm root cause and verification rules.
- Packaging Standard — confirm protection method and label format.

Level 2: Job Record Evidence
- PO + Order Confirmation — match part, qty, and ship date.
- Controlled Drawing PDF — match revision code and notes.
- Traveler / Router — verify operations, sign-offs, and timestamps.
- Material Certificates (MTR/MTC/CoC) — verify heat/lot and spec.
- Material Issue Log — prove heat/lot stays linked to the job lot.
- Setup Verification Sheet — prove first-piece checks with gauge IDs.
- In-Process Inspection Sheets — require numeric values and times.
- FAI / ISIR Pack — require ballooned drawing and results.
- Final Inspection Report — tie AQL plan to the shipment lot.
- Gauge Calibration Certificates — match gauge ID and due date.
- Deviation / Concession Record — verify approval and limits.
- NCR Record — show defect, containment, and affected lot.
- CAPA Closure Record — show verification that fixes worked.
The Essential 25 in a buyer-friendly table
I still like tables for evaluation. So I use clear headers for Google and buyers.
Also, I keep each row tied to “what I verify in two minutes.”
Level 1 table: System Control Documents
| Item No. | Document Name | Key Verification Point | Buyer Outcome |
|---|---|---|---|
| 1 | ISO 9001 Certificate | scope, site, expiry | proves baseline discipline |
| 2 | Quality Manual | matches real flow | reduces “poster ISO” risk |
| 3 | Document Control Procedure | revision release control | prevents drawing drift |
| 4 | Record Retention Procedure | integrity and access | supports audits and claims |
| 5 | Training Matrix | station coverage | reduces operator errors |
| 6 | Incoming Inspection Standard | sampling and criteria | blocks bad material early |
| 7 | Traceability Procedure | heat/lot + labels | stops material mix-ups |
| 8 | Material Control Procedure | receiving + issue logs | keeps tags alive |
| 9 | Calibration Procedure | intervals + standards | protects measurement trust |
| 10 | NCR Procedure | containment workflow | limits escaped defects |
| 11 | CAPA Procedure | root cause + verify | proves learning happens |
| 12 | Packaging Standard | protection + markings | prevents transit damage |
Level 2 table: Job Record Evidence
| Item No. | Document Name | Key Verification Point | Hard Link I check |
|---|---|---|---|
| 13 | PO + Order Confirmation | part, qty, date | matches packing list |
| 14 | Controlled Drawing PDF | revision code | matches traveler header |
| 15 | Traveler / Router | ops + sign-offs | matches process flow |
| 16 | Material Certificates | heat/lot + spec | matches lot label |
| 17 | Material Issue Log | heat → job lot | matches traveler lot |
| 18 | Setup Verification Sheet | first-piece values | includes gauge ID |
| 19 | In-Process Inspection | numeric data + time | shows inspector name |
| 20 | FAI / ISIR Pack | balloon + results | covers CTQ dimensions |
| 21 | Final Inspection Report | AQL reference | ties to shipment lot |
| 22 | Calibration Certificates | gauge ID + due | matches inspection sheet |
| 23 | Deviation Record | approval + limits | ties to NCR if needed |
| 24 | NCR Record | defect + containment | ties to affected lot |
| 25 | CAPA Closure | verify effectiveness | shows follow-up evidence |
How I audit a supplier in 30 minutes using one pack
I do not request 25 separate PDFs first. Instead, I request one unedited pack.
Then I run a hard-link audit. So I can approve or reject quickly.
My 10-step hard-link method
| Step | What I open | What must match | Why I care |
|---|---|---|---|
| 1 | PO + packing list | part number, qty | anchors the shipment |
| 2 | Drawing PDF | revision + notes | prevents silent changes |
| 3 | Traveler header | same revision | proves correct shop input |
| 4 | Material cert | heat/lot + spec | proves correct material |
| 5 | Material issue log | heat → job lot | blocks mixed lots |
| 6 | Setup sheet | first-piece values | proves launch control |
| 7 | In-process sheets | values over time | proves ongoing checks |
| 8 | FAI / ISIR | balloon + results | proves baseline capability |
| 9 | Calibration certs | gauge ID + due | proves measurement integrity |
| 10 | Label photo | lot code linkage | ties paper to boxes |
I also compare dates across the pack. Then I look for gaps and backfills.
Finally, I ask one question: “Can you trace one part to one heat number?”

Red flags that tell me the quality system is fake
I see the same tricks again and again. So I keep a short red-flag list.
If I hit two red flags, I stop the qualification.
My top red flags
- Every reading equals nominal value.
- Every handwriting line looks identical.
- Inspection sheets show only “OK.”
- Calibration due dates do not cover inspection dates.
- Heat numbers appear only on the material cert.
- NCR exists, but CAPA shows no verification.
Bad report vs Prime-style report
| What I see | Bad sign | Prime-style sign | What it tells me |
|---|---|---|---|
| Inspection entries | checkmarks only | numeric values | measurement actually happened |
| Handwriting | too uniform | mixed shift handwriting | real-time data entry |
| Corrections | “perfect” sheet | signed corrections | controlled reality |
| Gauge reference | missing | gauge ID listed | traceable measurement |
| Traceability | no lot linkage | lot + heat visible | audit trail works |
Process-specific pain points I verify
Different processes fail in different ways. So I change my audit questions.
That approach helps me catch hidden risks early.
Stamping: I verify coil heat numbers before the first strike.
CNC: I verify the exact gauge ID used for tight bores.
Casting: I verify melt batch traceability into the machining lot.
A real failure story that earned buyer trust
I do not fake perfection. Instead, I document reality so you sleep better.
So here is one case where we messed up, and fixed it fast.
On one export order, we shipped 304 stainless welded brackets. One customer found 0.5mm burr scratches inside the mounting hole during assembly. So we opened an NCR the same day.
First, I contained the lot in our warehouse. Then I traced the issue to a deburr wheel change log missing a signature. Also, I found one skipped in-process check on that shift.
Then we shipped replacement parts fast. And we added a checkpoint after wheel changes.
Finally, we updated the control plan and retrained that station.

What I expect inside an NCR/CAPA package
| Section | What I include | What you should see |
|---|---|---|
| Containment | quarantine lot code | stop-ship evidence |
| Root cause | 5-Why notes | specific, not vague |
| Corrective action | added checkpoint | updated control plan |
| Verification | follow-up data | defect trend drops |
| Communication | dated updates | fast, clear replies |
PPAP without paperwork overload
Some buyers require PPAP elements, especially automotive. Others only need core proof.
So I scale PPAP depth to part risk and tolerance.
I start with “light PPAP.” Then I expand after stable pilot lots.
Also, I keep all PPAP evidence tied to the Job Record Pack.
Practical PPAP map for custom metal parts
| PPAP element | When I use it | What I deliver | Where it links |
|---|---|---|---|
| Control Plan | always | CTQs + frequency | in-process records |
| PFMEA | medium/high risk | real failure modes | control plan actions |
| FAI / ISIR | new or changed parts | balloon + results | job record pack |
| MTR/MTC/CoC | always | heat/lot certs | traceability pages |
| Gauge control | tight tolerances | calibration proofs | inspection sheets |
Material traceability tables buyers use in real decisions
Many buyers search “quality” and really mean “material control.” So I address it directly.
I use simple comparison tables. Then I enforce heat/lot links in every pack.
Material comparison for qualification
| Material | Common use | Key cert field I verify | Common risk |
|---|---|---|---|
| SPCC / mild steel | stamping brackets | thickness + heat | mixed coils |
| 304 stainless | plates, brackets | chemistry limits | wrong grade |
| 6061-T6 aluminum | CNC housings | temper marking | temper mismatch |
| Alloy steel bar | shafts | heat + size | mixed bundles |
| Ductile iron | casting parts | batch + tensile | batch split drift |
Traceability by process step
| Step | Stamping | CNC | Casting | What I verify |
|---|---|---|---|---|
| Receiving | coil tag | bar tag | melt batch ID | tag photo exists |
| Issue to job | coil issue log | cut bundle log | batch release log | lot stays intact |
| In-process | bend angle checks | bore checks | key dims checks | numeric values |
| Final release | lot release | lot release | batch release | matches labels |
| Packing | carton lot code | carton lot code | pallet batch code | label photo proof |
A stronger challenge CTA for buyers
Stop gambling with your first order. Does your supplier’s paperwork look too clean?
Compare it to what you have on your desk right now.
Why Prime builds around buyer proof
I run Prime as a B2B wholesale factory, not a brochure company. So I optimize for buyer audits.
We founded Prime in 1993. Also, we run 10 production lines for metal components.
And we hold ISO international quality certification, because consistency matters.
I support stamping parts, CNC parts, welding parts, casting parts, fasteners, and plastic parts.
Also, I export to North America, Europe, the Middle East, and Australia.
So I design records and packaging for long-distance reliability.
FAQs
What are the essential quality documents to request from a new supplier?
I request one unedited Job Record Pack first. Then I verify ISO, traceability, inspection data, and calibration proof.
How do I verify a supplier quality system using a real shipment record package?
I trace PO → drawing revision → heat number → in-process data → calibration cert → shipment label. Then I check dates and signatures.
What should a Job Record Pack include for stamping parts?
It should include coil heat numbers, material issue logs, setup checks, and in-process bend data. Also, it should tie to carton lot codes.
What should a Job Record Pack include for CNC tight-tolerance parts?
It should include numeric values, gauge IDs, and calibration certificates for those gauges. Also, it should include FAI for first runs.
What should a Job Record Pack include for casting parts?
It should include melt batch traceability and material test evidence. Then it should link batch to machining lots and shipment labels.
What red flags mean the supplier backfilled inspection sheets?
I watch for identical handwriting, perfect nominal values, and “OK-only” sheets. Also, I watch for missing gauge IDs.
How should I evaluate NCR and CAPA quality?
I check containment speed, root cause specificity, and verification evidence. Then I check if the control plan changed.
Do I need PPAP for custom metal parts?
Automotive often requires PPAP elements. Many buyers start with light PPAP for pilot lots. So I scale it to risk.
What packaging documents matter most for export orders?
I ask for packaging standards, label standards, and packing photos. Then I verify separators and moisture protection.
Conclusion
I qualify suppliers with one unedited Job Record Pack, because it proves shop-floor truth.
If you want stable quality and fast delivery, send your drawing now.
Want to verify a supplier fast—without guessing?
If you want a clearer view of how we control measurement, traceability, and final release, visit our Quality Inspection “tank page” here:





